Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124
Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124
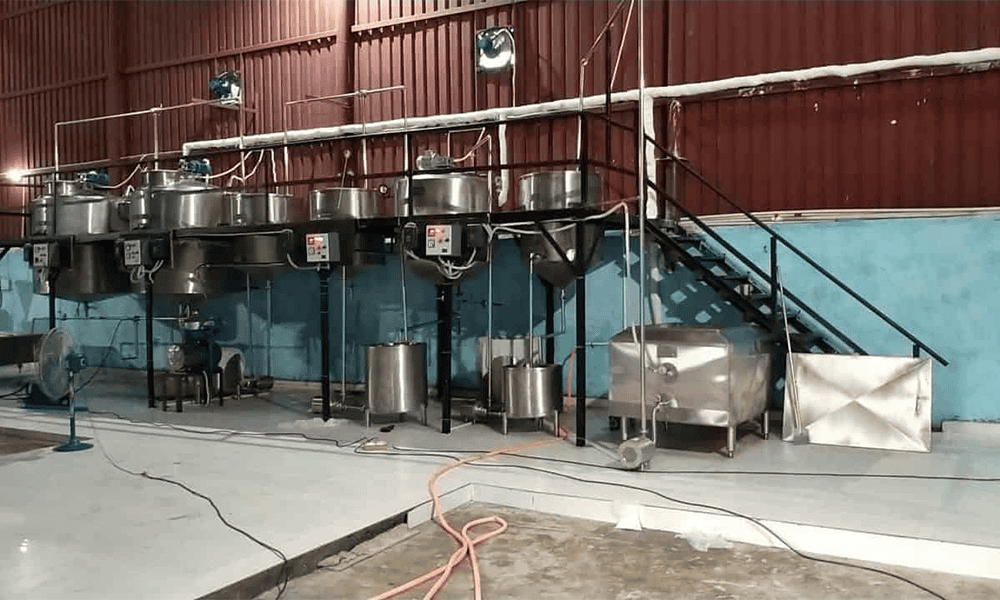
Ghee production is relevant to retail brands, restaurants, food-service companies, and industrial food manufacturers. As production volumes increase, manual methods may not provide the process control needed for consistent commercial output.
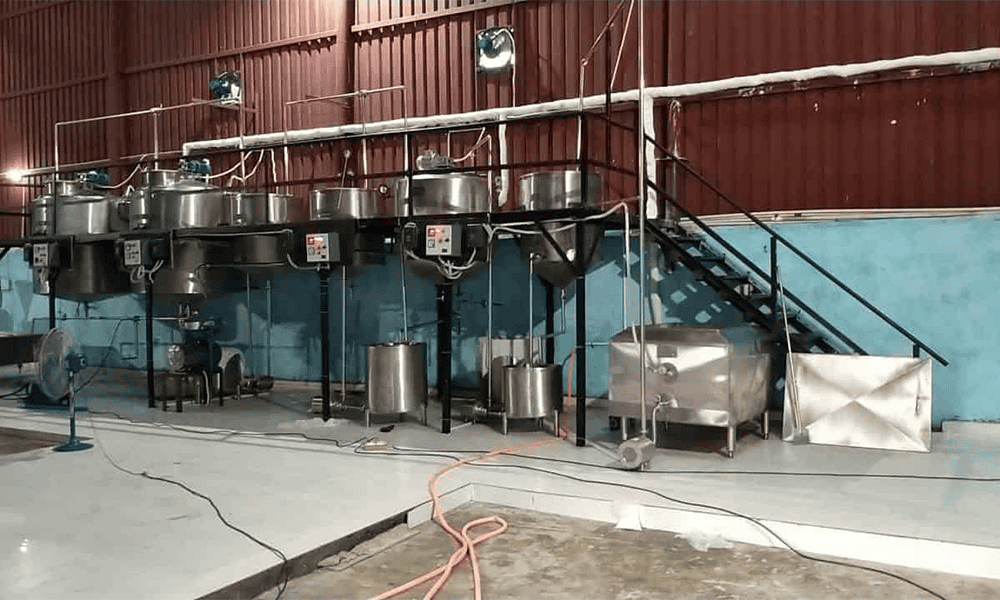
A modern Ghee Plant provides an organised route for processing dairy fat, controlling heat, separating non-fat components, filtering the product, and preparing it for packaging.
Why Commercial Process Design Matters
Ghee quality can be affected by raw-material condition, heating, clarification, filtration, storage, and packaging. Commercial processing therefore needs a controlled sequence.
The broad production route can be described as:
Dairy-Fat Reception → Preparation → Heating → Moisture Removal → Clarification → Filtration → Storage → Filling → Final Packing
The exact operating conditions depend on the selected process and product requirements.
Key Processing Equipment
The main equipment groups may include:
Equipment should be sized as a complete system. For example, increasing processing capacity without increasing storage or packaging capacity can create a bottleneck.
Raw Material Management
Good manufacturing begins with controlled raw-material handling. Receiving procedures should identify incoming materials and provide suitable storage before processing.
The raw material selected for the process affects melting, heating, clarification, and overall equipment requirements.
Businesses should establish raw-material specifications and acceptance procedures appropriate to their product.
Heating and Clarification
Controlled heating supports moisture removal and separation of non-fat milk components. The process should be monitored according to the established production specification.
Clarification is important because it separates unwanted material from the dairy fat. Filtration can then provide an additional separation stage before the product reaches the finished-product tank.
Storage and Packaging
Finished ghee may be held in hygienic tanks before packaging. Storage capacity should be matched with production batches and packaging schedules.
Packaging options can include:
The chosen system should provide accurate filling and effective sealing while protecting the product during storage and distribution.
Quality Assurance
A commercial manufacturer should establish written specifications and testing procedures.
Depending on the product, quality control may cover:
Batch records can improve traceability and make it easier to investigate quality variations.
Hygiene and Factory Design
The factory should separate major activities logically. Raw-material receiving, processing, packaging, and finished-goods storage should be arranged to support hygienic movement.
Equipment should allow inspection and cleaning. Sanitary pipelines, accessible valves, suitable drainage, and appropriate cleaning procedures can reduce operational problems.
A CIP system can be included where it fits the plant’s size and process design.
USA Requirements
US-bound businesses should review the applicable FDA food-safety framework. FDA’s FSMA framework includes hazard analysis, preventive controls, monitoring, verification, and recordkeeping requirements for covered facilities.
Therefore, process documentation and food-safety planning should be considered alongside machinery selection.
UK Requirements
A UK-focused facility should consider applicable food hygiene and food-information requirements. Product labels, allergens, packaging, batch identification, and storage information should be planned according to the product and sales format.
Australia Requirements
Businesses supplying Australia should review the applicable Food Standards Code. FSANZ confirms that the Code covers general labelling and information requirements as well as product-specific requirements.
The processing and packaging system should be capable of supporting the selected product specification.
New Zealand Requirements
New Zealand has a specific regulatory structure for dairy processing. MPI states that dairy products for export must meet New Zealand food-safety requirements and destination-market requirements, with applicable products manufactured and stored under a registered RMP or other permitted programme.
Businesses should therefore consider export documentation, traceability, and destination requirements during project planning.
UAE Requirements
For the UAE, product registration, import requirements, labelling, packaging, and distribution conditions should be reviewed. Businesses should also consider high ambient temperatures when selecting packaging and planning storage.
South Africa Requirements
South African projects should be assessed against the applicable food and dairy framework. Processing controls, sanitation, packaging, storage, and traceability should form part of the facility plan.
Canada Requirements
For Canada, businesses should consider the applicable dairy-product standards, preventive controls, food-safety requirements, packaging, and labelling. Importers and manufacturers should verify current requirements for the exact product.
Automation and Monitoring
Automation can improve process consistency by monitoring temperature, tank levels, transfer operations, filling, and other selected parameters.
A smaller producer may use partial automation, while a larger commercial operation may integrate several processing stages into a central control system.
FAQs
1. What is the purpose of a commercial Ghee Plant?
It provides controlled equipment and process stages for converting suitable dairy fat into ghee and preparing the finished product for commercial packaging.
2. Which factors affect ghee production capacity?
Raw-material supply, batch size, heating time, operating hours, storage volume, filtration rate, and packaging speed all influence practical production capacity.
3. What role does filtration play?
Filtration helps remove remaining suspended material following clarification, supporting a cleaner and more consistent finished product.
4. How can businesses prepare for international sales?
They should identify target countries early, review applicable food and packaging requirements, define product specifications, establish traceability, and select equipment that supports the intended packaging and production model.
Conclusion
A well-planned Ghee Plant connects processing technology with hygiene, quality control, storage, packaging, and market requirements. Businesses should define their production objectives before choosing equipment so that every part of the facility works together.
NK Dairy Equipments LLP is an India-based manufacturer and exporter of dairy processing equipment, supplying solutions for dairy processing applications in the USA and international markets.
Learn More About Ghee Processing Solutions:
Explore Ghee Plant solutions, equipment options, process flow, and commercial setup requirements with NK Dairy Equipments LLP.
Visit: https://nkdairyequipments.com/ghee-plant/
Contact NK Dairy Equipments LLP for suitable dairy processing solutions for your market and production requirements.