Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124
Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124
Specialty silica has become an important material across numerous industrial sectors because of its distinctive physical and chemical properties. Its ability to improve product strength, stability, texture, durability, and performance makes it valuable in applications ranging from automotive manufacturing and construction to personal care, pharmaceuticals, food processing, and electronics. As industries continue to focus on product quality, manufacturing efficiency, and advanced material development, the demand for specialized silica solutions is receiving greater attention.
The specialty silica market is shaped by changing industrial requirements, technological improvements, and the growing need for materials that deliver consistent performance. Manufacturers are exploring different production methods, particle structures, and surface treatments to develop products suitable for specific applications. Understanding these developments is essential for businesses seeking to identify emerging opportunities and strengthen their competitive position.
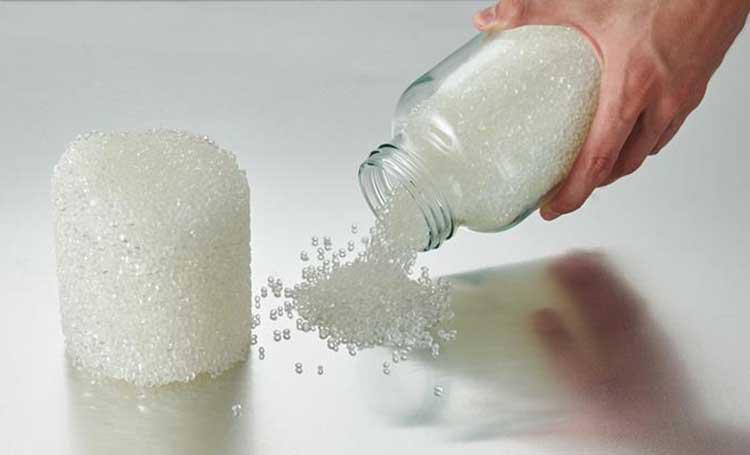
Specialty silica refers to engineered forms of silicon dioxide designed to provide particular functional characteristics. Unlike conventional silica, these materials are manufactured to meet specific performance requirements, including controlled particle size, porosity, surface area, and absorption capacity.
Common varieties include precipitated silica, fumed silica, silica gel, and colloidal silica. Each type serves different industrial purposes. Precipitated silica is widely used in rubber products, particularly tires, while fumed silica provides thickening, reinforcing, and stabilizing properties in coatings, adhesives, and sealants.
Silica gel is valued for moisture absorption, making it useful in packaging and storage applications. Colloidal silica supports precision polishing, surface treatment, and specialized manufacturing processes. These different product characteristics allow manufacturers to serve diverse industries with customized material solutions.
One of the important areas of research is the expanding use of specialty silica across established and emerging industries. The automotive sector represents a significant application area, particularly because of the increasing focus on tire performance, rolling resistance, and durability.
Precipitated silica is used in tire compounds to support improved traction and reduced rolling resistance. As vehicle manufacturers and tire producers explore technologies that improve energy efficiency, demand for specialized rubber additives is expected to remain relevant.
The construction industry also creates opportunities through applications in cement, concrete, coatings, and sealants. Specialty silica can improve mechanical strength, resistance, and consistency in selected formulations. Meanwhile, the personal care industry uses specific silica grades in cosmetics, skincare formulations, and oral care products because of their texturizing, absorbing, and polishing properties.
Pharmaceutical and food-processing applications provide additional areas of interest. Carefully selected silica grades can function as flow agents, anti-caking ingredients, and formulation aids, subject to applicable safety and quality requirements.
Technological advancement is an important research area within specialty silica production. Manufacturers are investing in improved processing techniques to achieve greater control over particle characteristics, product purity, and functional performance.
Innovations in surface modification are particularly relevant because they allow silica to interact more effectively with different materials. Modified silica products can support better compatibility with polymers, coatings, and other chemical formulations.
Research into nanoscale materials is also creating new possibilities. Silica particles with carefully controlled structures can contribute to advanced coatings, electronic components, specialty adhesives, and precision manufacturing applications.
Automation and digital process monitoring are further transforming production facilities. Advanced equipment helps manufacturers monitor processing conditions, maintain product consistency, and identify operational inefficiencies. These improvements can support better resource utilization while reducing variations between production batches.
Environmental responsibility has become an increasingly important consideration for specialty silica manufacturers. Industrial customers are paying greater attention to production efficiency, energy consumption, waste management, and the environmental characteristics of raw materials.
Manufacturers are exploring production processes that reduce water usage, optimize energy requirements, and improve material recovery. Efficient manufacturing can help lower operating expenses while supporting broader sustainability objectives.
Another important development involves the use of specialty silica in products designed to improve resource efficiency. For example, silica-enhanced tire compounds can contribute to lower rolling resistance, potentially supporting improved vehicle energy efficiency when incorporated into suitable tire designs.
However, sustainability improvements require careful evaluation of the entire production lifecycle. Manufacturers must balance environmental objectives with product performance, cost considerations, and regulatory requirements.
Despite its diverse applications, the specialty silica industry faces several operational and commercial challenges. Raw material availability, energy expenses, transportation costs, and manufacturing complexity can influence production economics.
Maintaining consistent product quality is another important consideration. Different applications require precise specifications, and even minor variations in particle size, surface properties, or purity may affect final product performance.
Regulatory compliance also requires attention, particularly in food, pharmaceutical, cosmetics, and other applications involving strict product standards. Manufacturers must invest in appropriate testing, documentation, and quality management systems.
Competition from alternative materials can create additional pressure. Depending on the application, customers may consider other reinforcing agents, fillers, or functional additives. Specialty silica producers therefore need to demonstrate measurable performance benefits while maintaining competitive pricing.
Competition within the specialty silica market is influenced by product innovation, manufacturing capacity, distribution networks, and relationships with industrial customers. Companies are focusing on developing application-specific grades instead of relying exclusively on standardized products.
Strategic partnerships with tire manufacturers, chemical companies, construction suppliers, and personal care producers can help silica manufacturers understand changing customer requirements. These relationships also support collaborative product development and long-term supply arrangements.
Geographical expansion is another strategy used by industry participants. Establishing production facilities closer to major industrial customers can improve delivery efficiency and strengthen regional market presence.
Investment in research and development remains important for maintaining product differentiation. Businesses that develop reliable, customized solutions may find opportunities in specialized applications where performance requirements are particularly demanding.
Future research is expected to focus on advanced silica formulations, improved manufacturing efficiency, and applications in emerging technologies. Electric vehicle components, advanced electronics, high-performance coatings, and next-generation construction materials could provide additional areas for product development.
The specialty silica market may also benefit from growing interest in lightweight materials and energy-efficient industrial solutions. However, the pace of adoption will depend on production costs, technical performance, customer acceptance, and investment conditions across end-use industries.
Manufacturers will need to monitor changing application requirements and invest in technologies that support consistent quality and sustainable operations. Greater collaboration between material producers and end users could also accelerate the development of specialized products.
Specialty silica continues to serve as an important functional material across a wide range of industrial applications. Its versatility, adaptability, and performance-enhancing characteristics create opportunities in automotive, construction, healthcare-related products, personal care, and advanced manufacturing. Although production costs, regulatory requirements, and competition present challenges, ongoing innovation and application-specific development can support further industry expansion. Companies that prioritize product quality, efficient manufacturing, and customer collaboration will remain active participants in the evolving specialty silica industry.